Ultra-pure & high-purity HDPE drum packaging — engineered and manufactured in Maumee, Ohio 419-897-9110
Quality & Capabilities

Quality you can qualify against.

A failed drum doesn’t just lose product. It contaminates a process, fails an audit, or stops a line. Every process in our Maumee plant exists to control that risk — and every control produces evidence you can file.
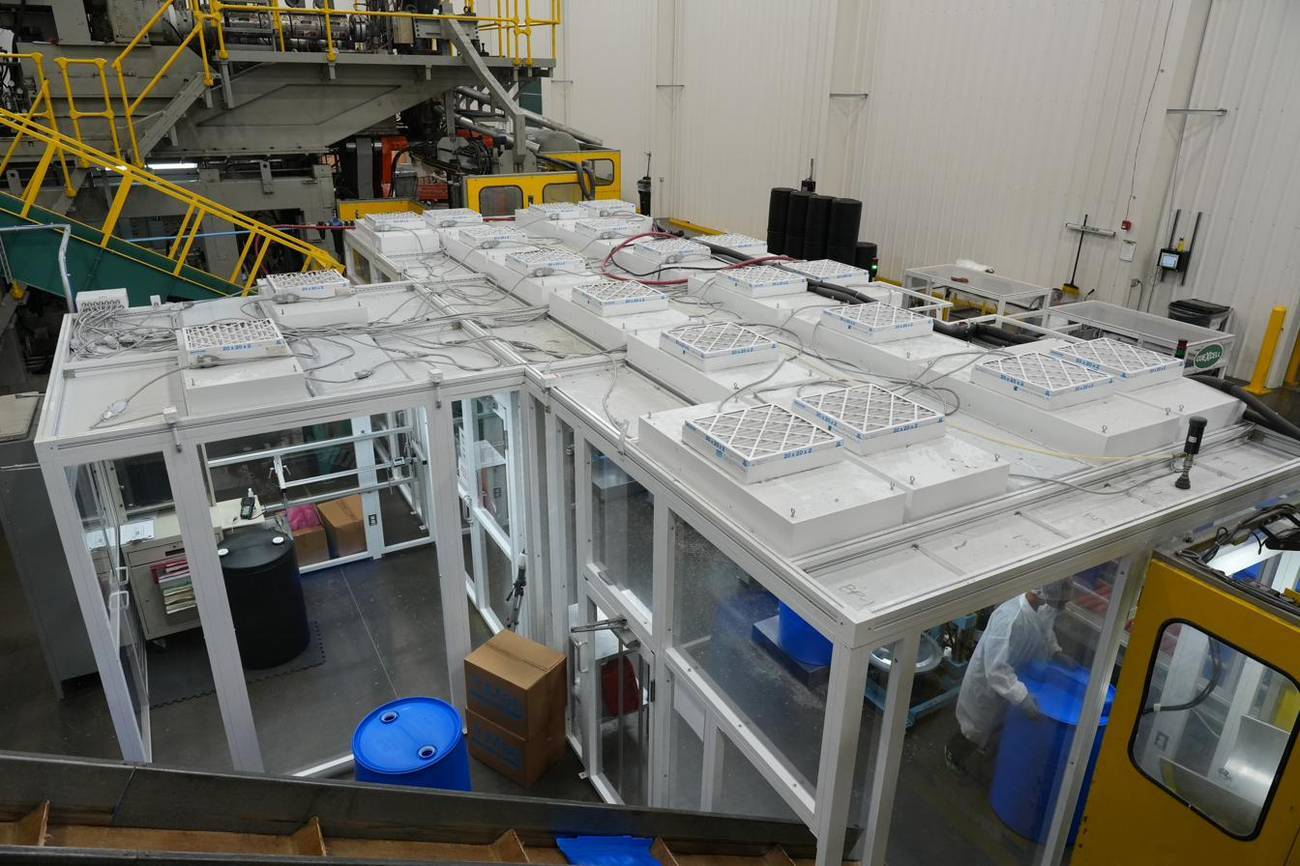
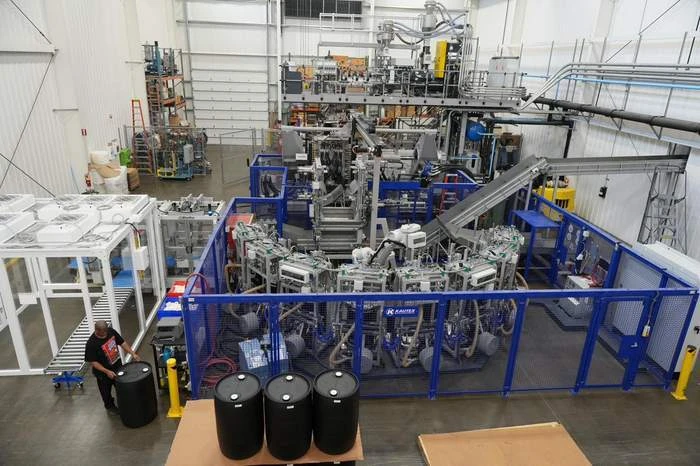
Overhead view of the clean-room enclosures and HEPA filter banks on the COEXCELL production floor
Clean-room finishing enclosures — Maumee, OH
The Process

From railcar to documented shipment.

Five stages, in the order they happen on our floor. For each: what’s controlled, how it’s controlled, and the evidence produced.
01
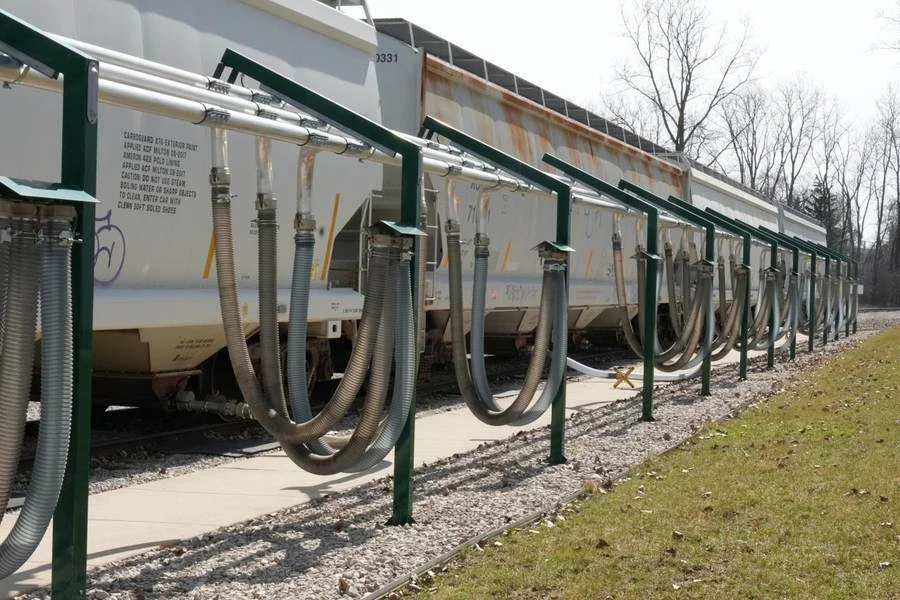
Railcars of HDPE resin at COEXCELL's dedicated unloading stations

Resin receiving

Controlled
Raw material identity and handling from the start of the process.
How
HDPE resin arrives by rail at dedicated unloading stations in our railyard and transfers to storage.
Evidence
Material receiving records.
02
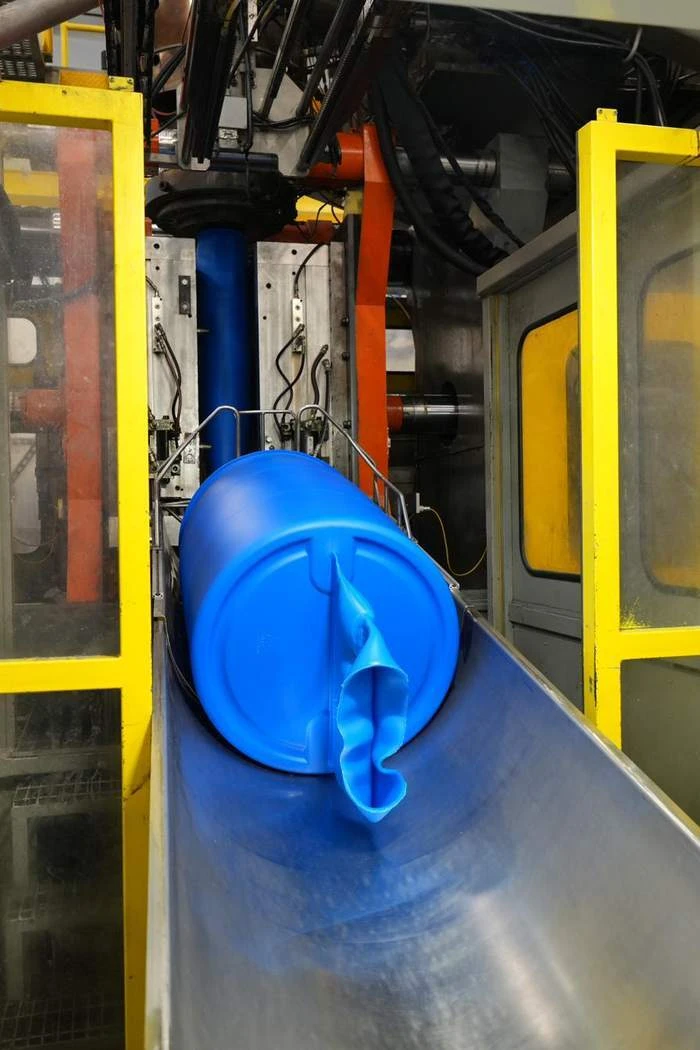
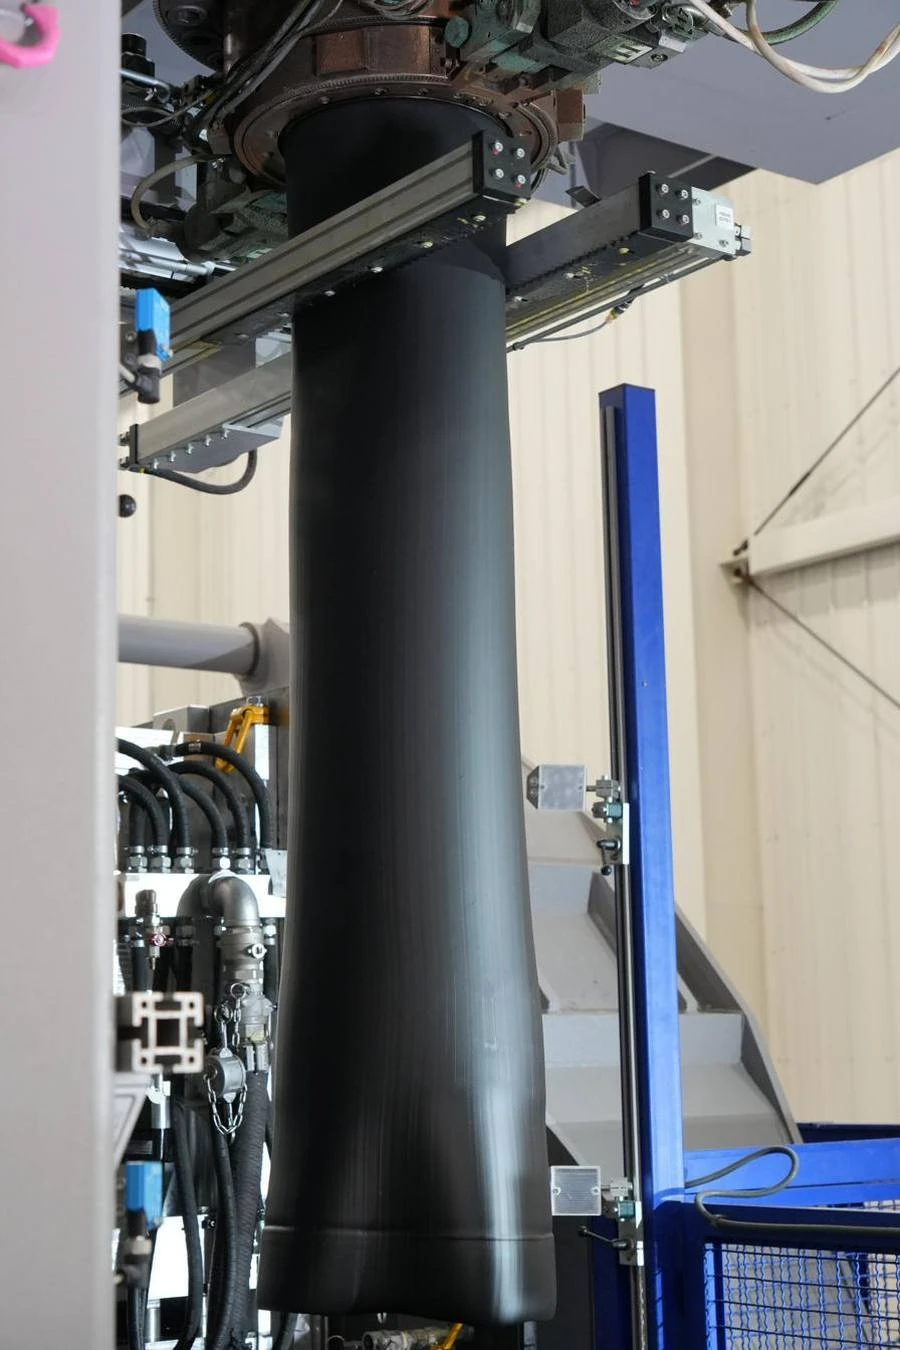
Coextruded HDPE parison descending from the die head before molding

Tri-layer coextrusion

Controlled
Layer structure and the purity of the product-contact surface.
How
Coextrusion isolates colorants and UV stabilizers in the exterior structure. A virgin ultra-clean resin forms the inner liner — the only surface the chemical touches. ICAS™ process controls apply during molding.
Evidence
Drum body weight confirms total material content. Wall-thickness measurement confirms thickness and layer distribution across the drum body.
03
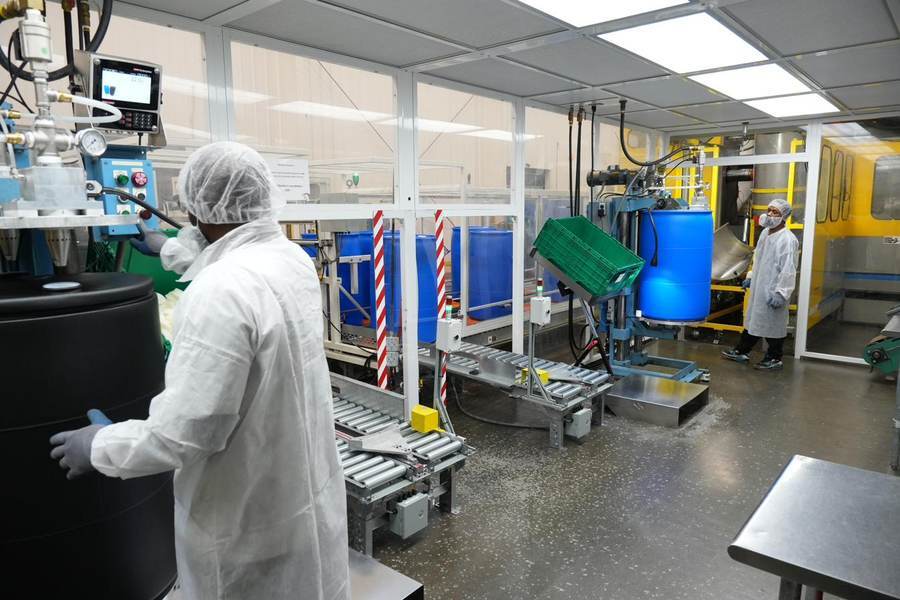
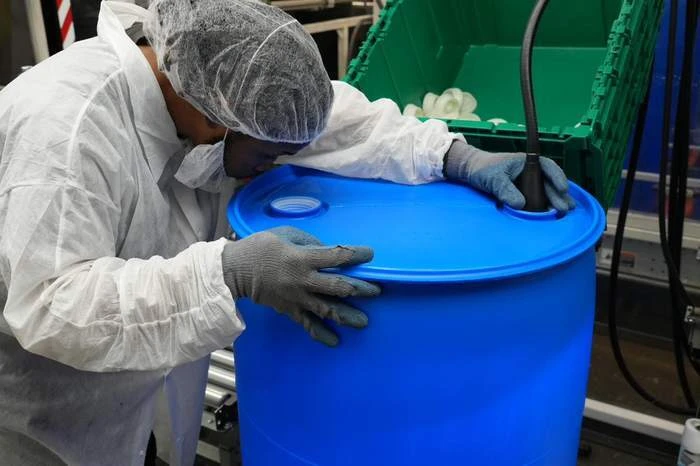
Gowned technicians finishing drums inside the enclosed clean-room area

Clean-room finishing

Controlled
Particle exposure while drums are finished, closed, and handled.
How
Drums move through enclosed Class 1000 clean-room areas with filtered air, handled by gowned technicians and automated equipment.
Evidence
Air quality readings are measured and recorded in the post-forming clean room. Drum cleanliness is verified downstream in the Class 100 liquid particle-count laboratory.
04
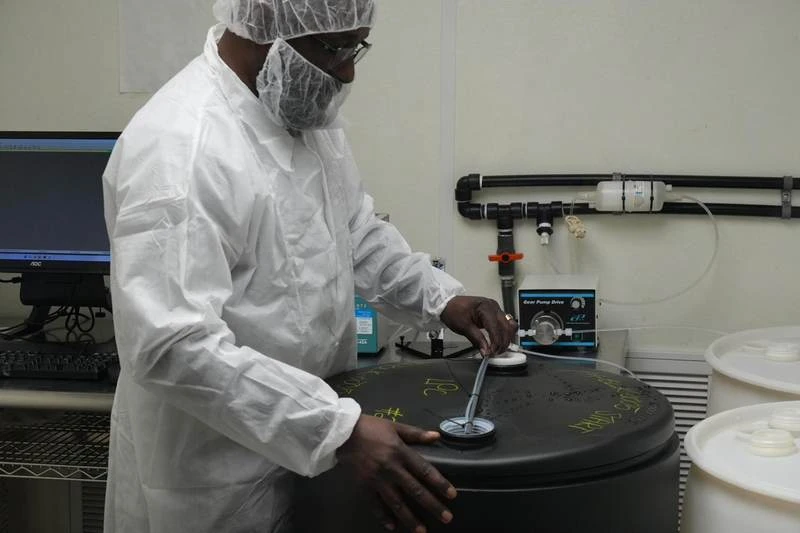
Technician in clean-room gowning running a liquid particle count on a drum

Testing & verification

Controlled
Containment, cleanliness, and transport performance of the finished drum.
How
Liquid particle counting, hydrostatic and leak checks, wall-thickness verification, and UN drop testing at certified heights.
Evidence
UN/DOT markings by model and configuration. Certification documents and test summaries are available per configuration.
05
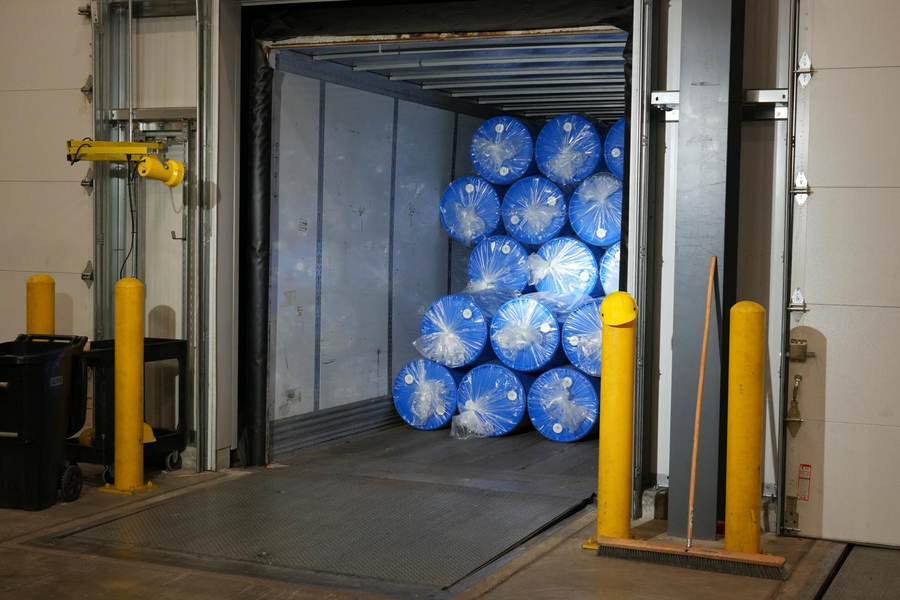
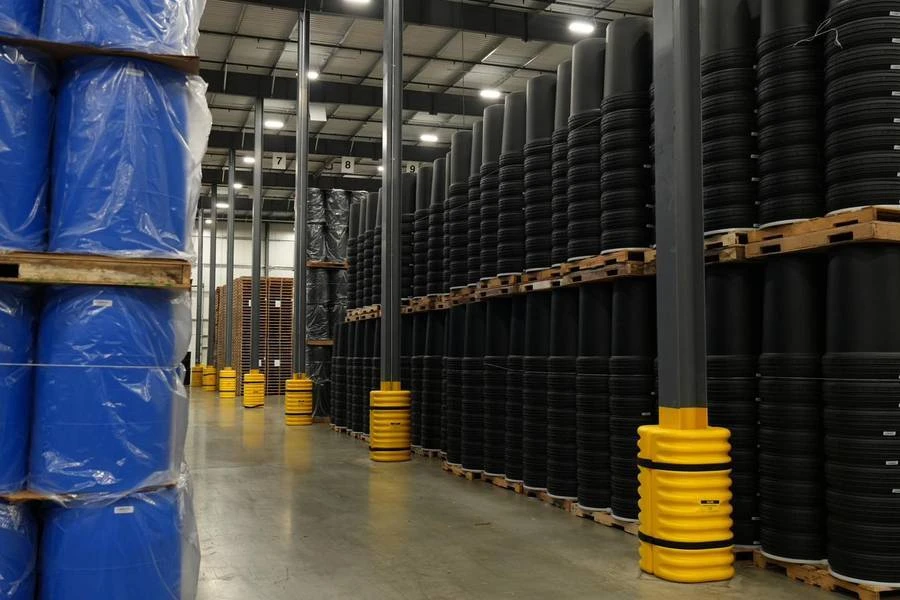
Palletized drums staged in a partially loaded trailer for shipment

Documented shipment

Controlled
The identity of what ships, and the paperwork that travels with it.
How
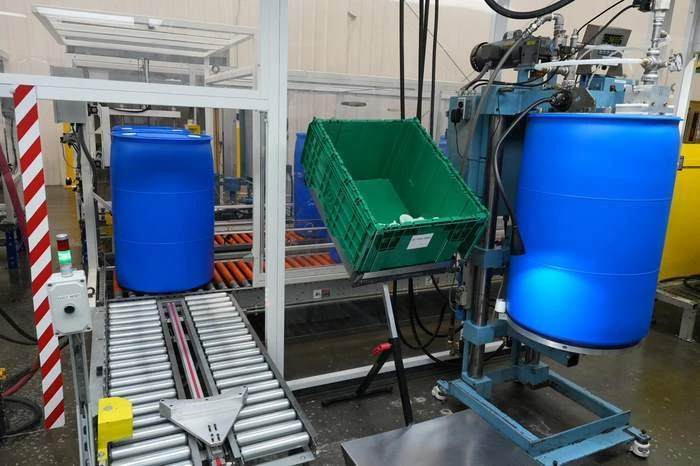
Finished drums are staged, palletized, and loaded on-site. Traceability labeling is applied by model — IC, K55, and C55UP drums each carry a unique traceability identification label.
Evidence
Shipment documentation, with certifications and data sheets supplied on request.

Certifications and test results are documented per model and configuration. We do not generalize an approval from one drum or configuration to another.

Documented Quality

Every claim has a test behind it.

Purity and performance statements are only useful when they’re documented. Our in-house laboratory and in-process checks generate documented evidence for every production lot.

Technician running a liquid particle count on a drum
Liquid Particle Count

Cleanliness is verified in our Class 100 LPC laboratory before drums ship.
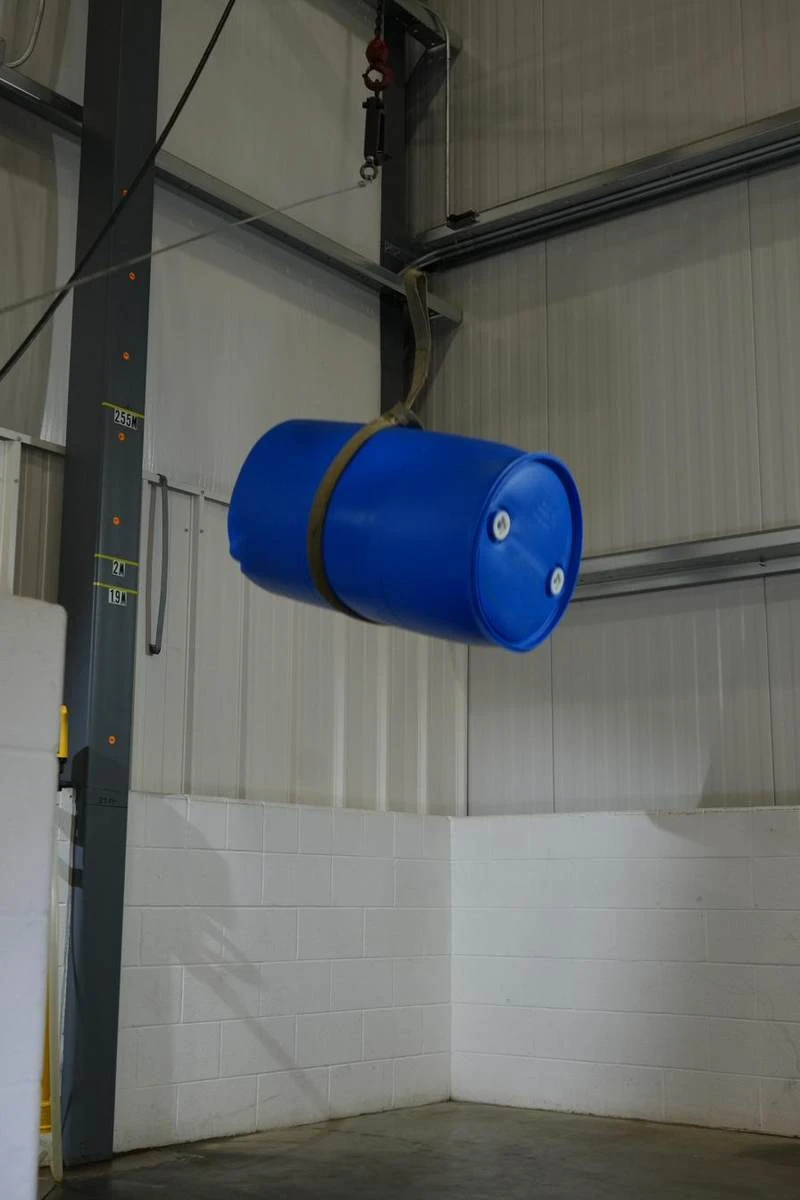
Drum suspended at a marked height in the drop-test area
UN Drop Testing

Drums are drop-tested at certified heights to support their UN/DOT markings.
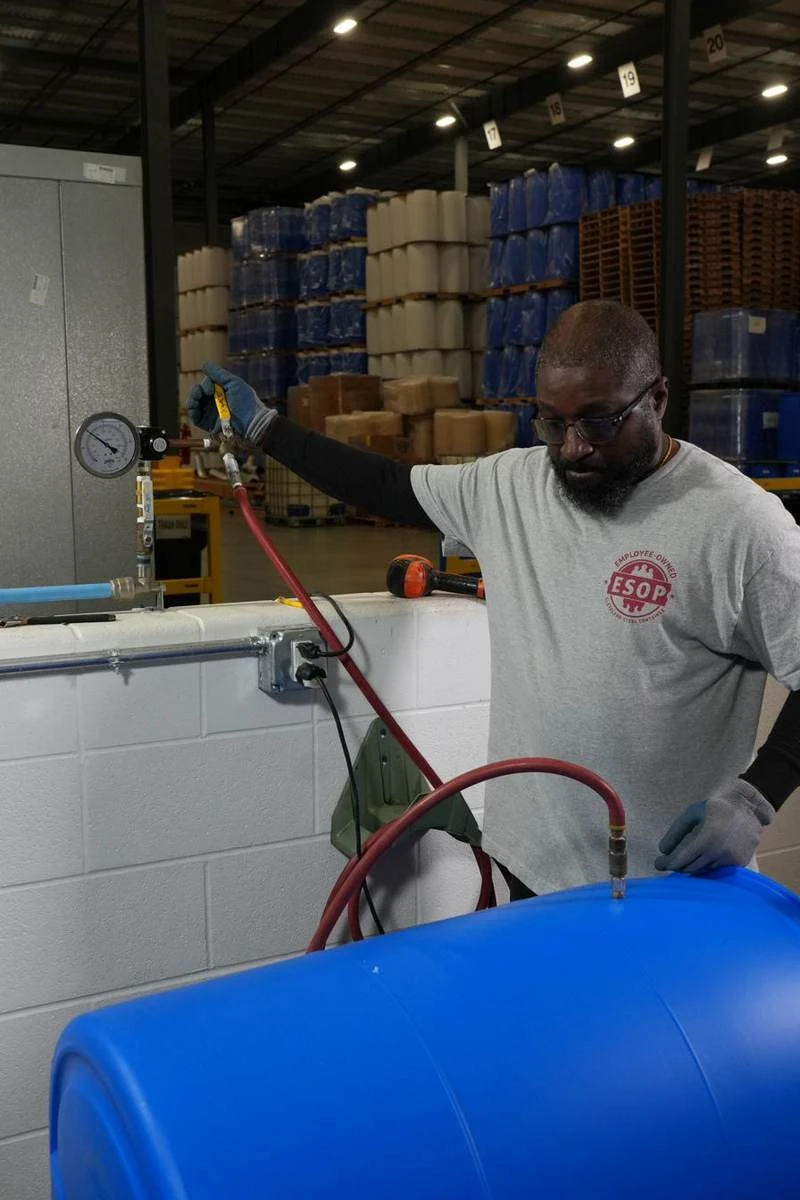
Technician performing a hydrostatic pressure test on a blue drum
Hydrostatic & Leak Testing

Pressure and leak checks confirm containment as part of routine verification.
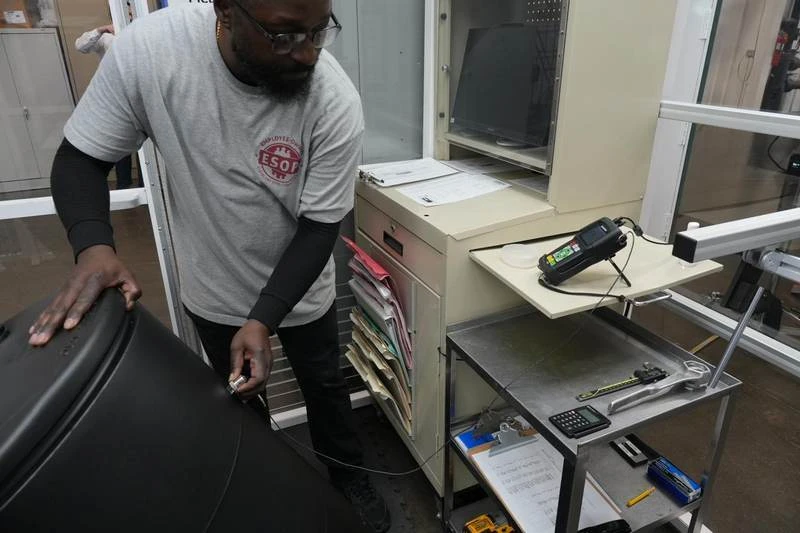
Technician measuring drum wall thickness with a handheld gauge
Wall Thickness Verification

Gauge measurement confirms wall thickness and layer distribution across the body.

Certification documents, technical data sheets, and test summaries are available for each drum configuration.

Request technical data
Purity, Stated Precisely

We keep purity claims specific — because you have to.

Particle counts, metal extractables, and clean-room classifications are different measurements. We state each on its own terms, per model, so your qualification paperwork can too.

Product-contact purity

Tri-layer construction isolates colorants and UV stabilizers in the exterior structure. The virgin inner liner — an ultra-clean resin — is the only surface the chemical touches.

Applies to: tri-layer models · verified by wall-thickness & LPC

Resin grades matched to your spec

Inner-layer resins are available in three high-purity grades — High Purity Standard, High Purity Plus, and Ultra-Pure Premium — across the ultra-pure models, so the drum is matched to your extractables requirement rather than a one-size claim.

Grade selection by Cleanliness is documented in our in-house Class 100 liquid particle-count laboratory testing.

Class 100 particle-count laboratory

In-house liquid particle-count laboratory verifying cleanliness.

In-house LPC lab · results per configuration

Certifications by model, never generalized

UN/DOT approvals are stated with their exact markings — 1H1/Y1.9/150, 300 kPa options, and X-rated Packing Group I configurations where certified. An approval for one configuration is never extended to another.

Exact markings on each product page

UN/DOT

Tested and certified by model and configuration — exact markings on each product page.

ISO 9001

Certified quality management system.

Class 1000 Clean Room

Post-forming finishing performed in a Class 1000 clean-room environment.

Class 100 LPC Lab

In-house liquid particle-count laboratory verifying cleanliness.

FDA-Compliant N55

The N55 nestable drum is FDA-compliant for food and beverage processing applications.

Next Step

Discuss your packaging requirements.

Tell us your purity, performance, and compliance requirements.

Or call  419-897-9110